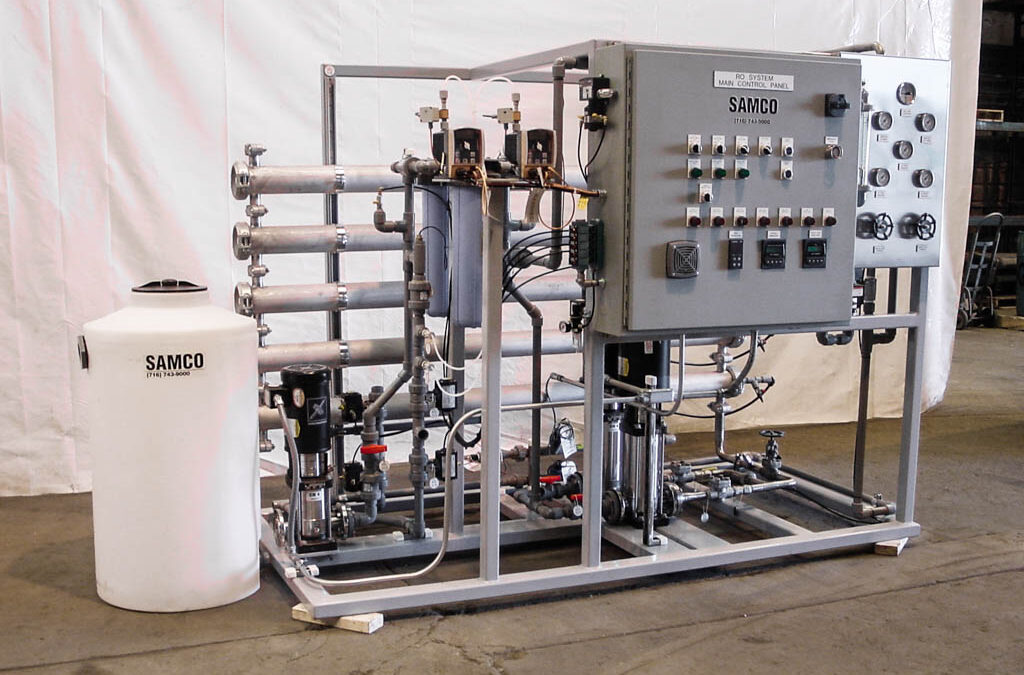
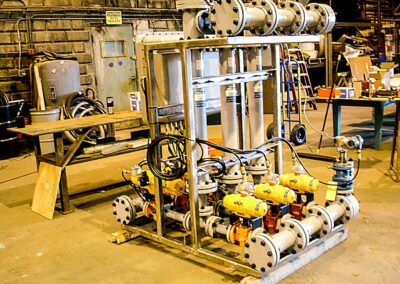
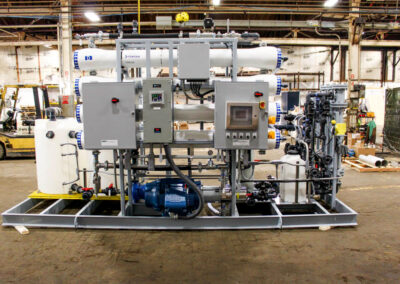
Project Briefs: Sulfuric Acid Plant Supports Plant Expansion With SAMCO Ultra-High Purity Reverse Osmosis System and Ion Exchange Polishing Project Overview A sulfuric acid plant in the Northeast required ultra-high purity water to feed its new product line in an...
Project Briefs: Oil Refinery Replaces Old Softening Equipment and Reduces Boiler Makeup Water Hardness with UPCORE™ Softening System Project Overview When an oil refinery in West Virginia needed to replace its softening equipment with a more efficient system, SAMCO...
Project Briefs: Major Food Manufacturer In Buffalo, NY, Works With SAMCO to Produce High-Purity Boiler Makeup Water Project Overview In order to minimize boiler blowdown requirements at a prominent food manufacturer/plant in Buffalo, NY, SAMCO helped the client...
Project Briefs: Methyl Ethyl Ketone Producer Leverages SAMCO Tube Filtration System for Efficient Reuse of Sulfuric Acid Process Stream Project Overview When a global producer of halobutyl rubber and methyl ethyl ketone sought a sulfuric acid filtration system for its...
Project Briefs: Oil Producer Sustains Offshore Operations by Leveraging SAMCO Reverse Osmosis Technology for Potable Water Generation at Sea Project Overview Located far offshore in the Gulf of Mexico, a large oil platform needed an efficient means of converting...